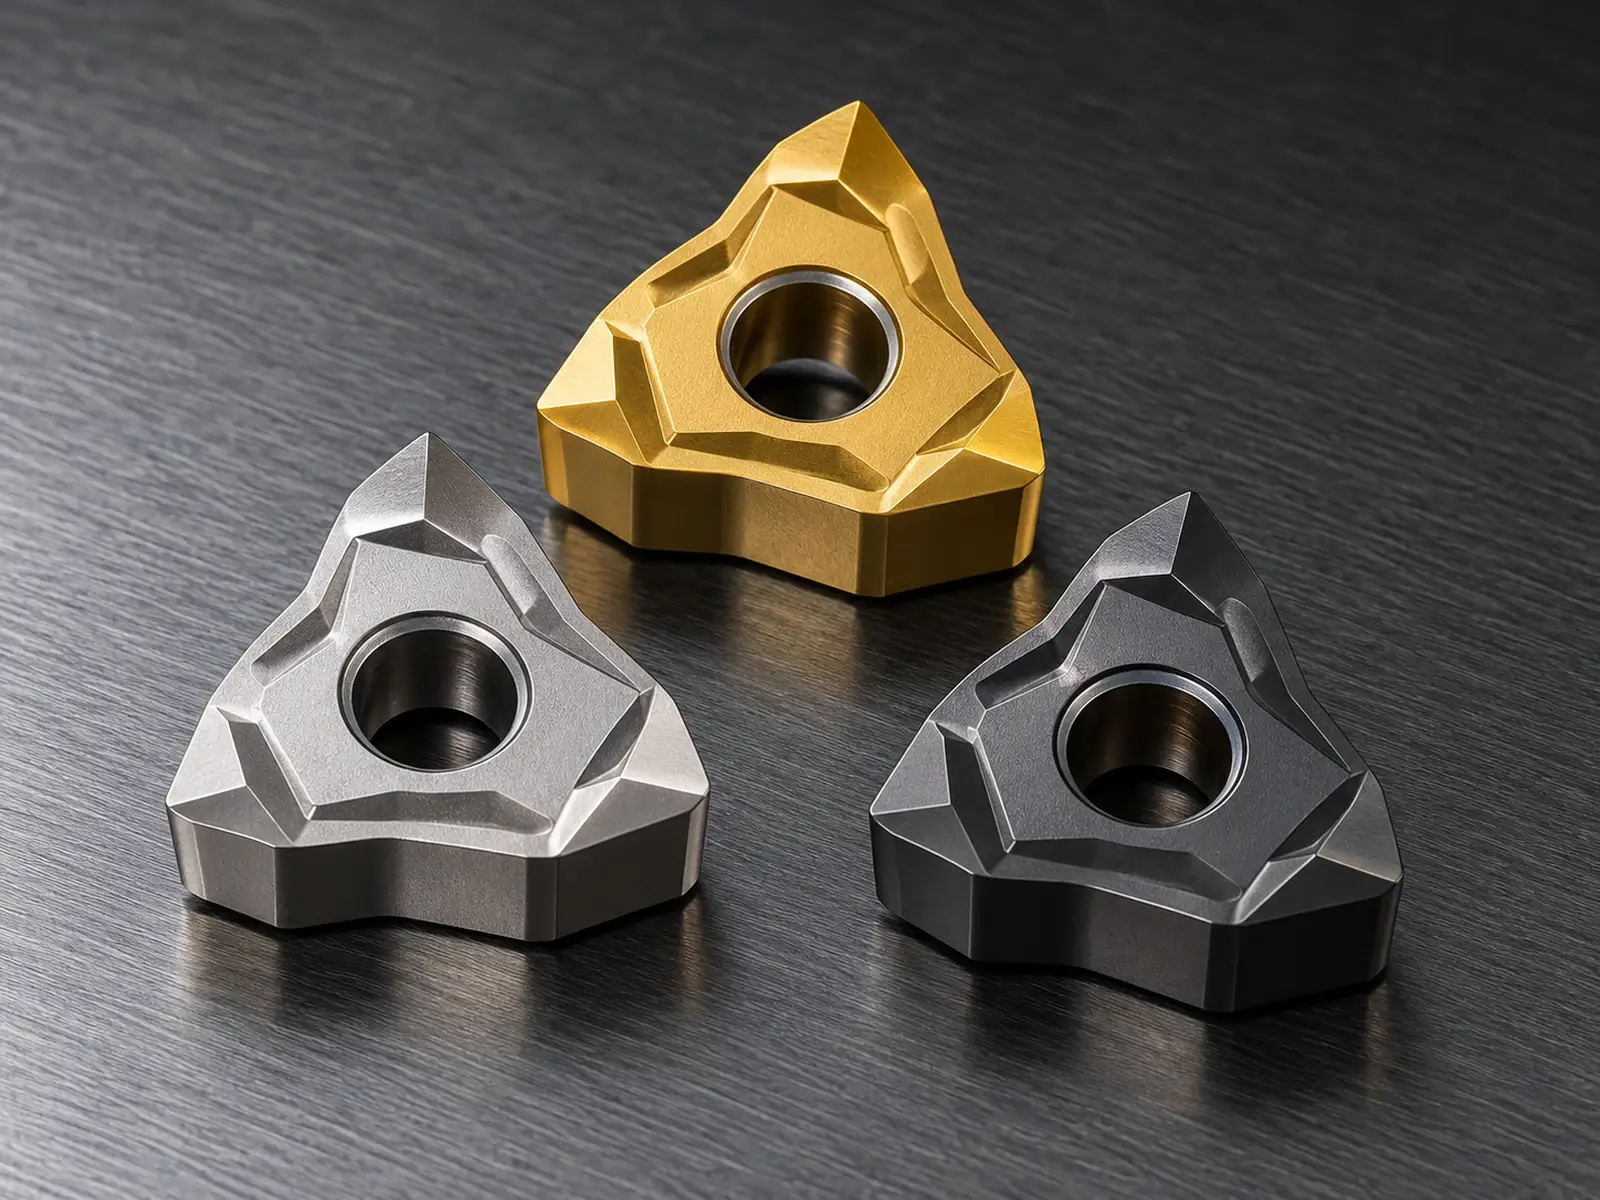
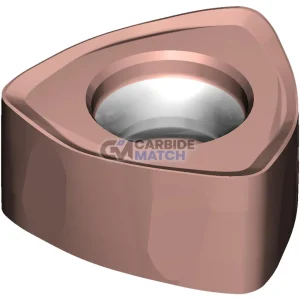
Source WNMU six-edge milling inserts for shoulder and face machining, with platform-specific dimensions, edge form and grade direction reviewed against the cutter body and work material.
WNMU is a trigon milling-insert family with nominal zero clearance, M-class tolerance and a double-sided fixing-hole configuration. Compatible cutter systems use six cutting edges for shoulder and face milling. The same nominal size can have different thicknesses, holes and seat geometry across platforms.
Key Specifications
Insert Shape80° trigon family
Clearance Angle0° nominal
Tolerance ClassM class
Insert ConfigurationDouble-sided with fixing hole; 6 cutting edges
Common ISO Sizes0403, 0504, 0604 and 0806
Primary ApplicationsSquare-Shoulder Milling, Face Milling, Slot Milling
Custom WNMU Insert Options
Configure the key manufacturing details for your insert application, from dimensions and cutting material to edge condition and identification.
Dimensions & Tolerances
Specify insert dimensions and tolerances according to your drawings.
Cutting Material & Grade
Select insert material and grade to suit your machining application.
Top Geometry & Chip Control
Customize top geometry and chip control features for your cutting needs.
Edge Preparation
Specify edge honing, chamfers and other edge preparation options.
Coating & Surface Treatment
Choose coating and surface treatments to meet your cutting needs.
Marking & Packaging
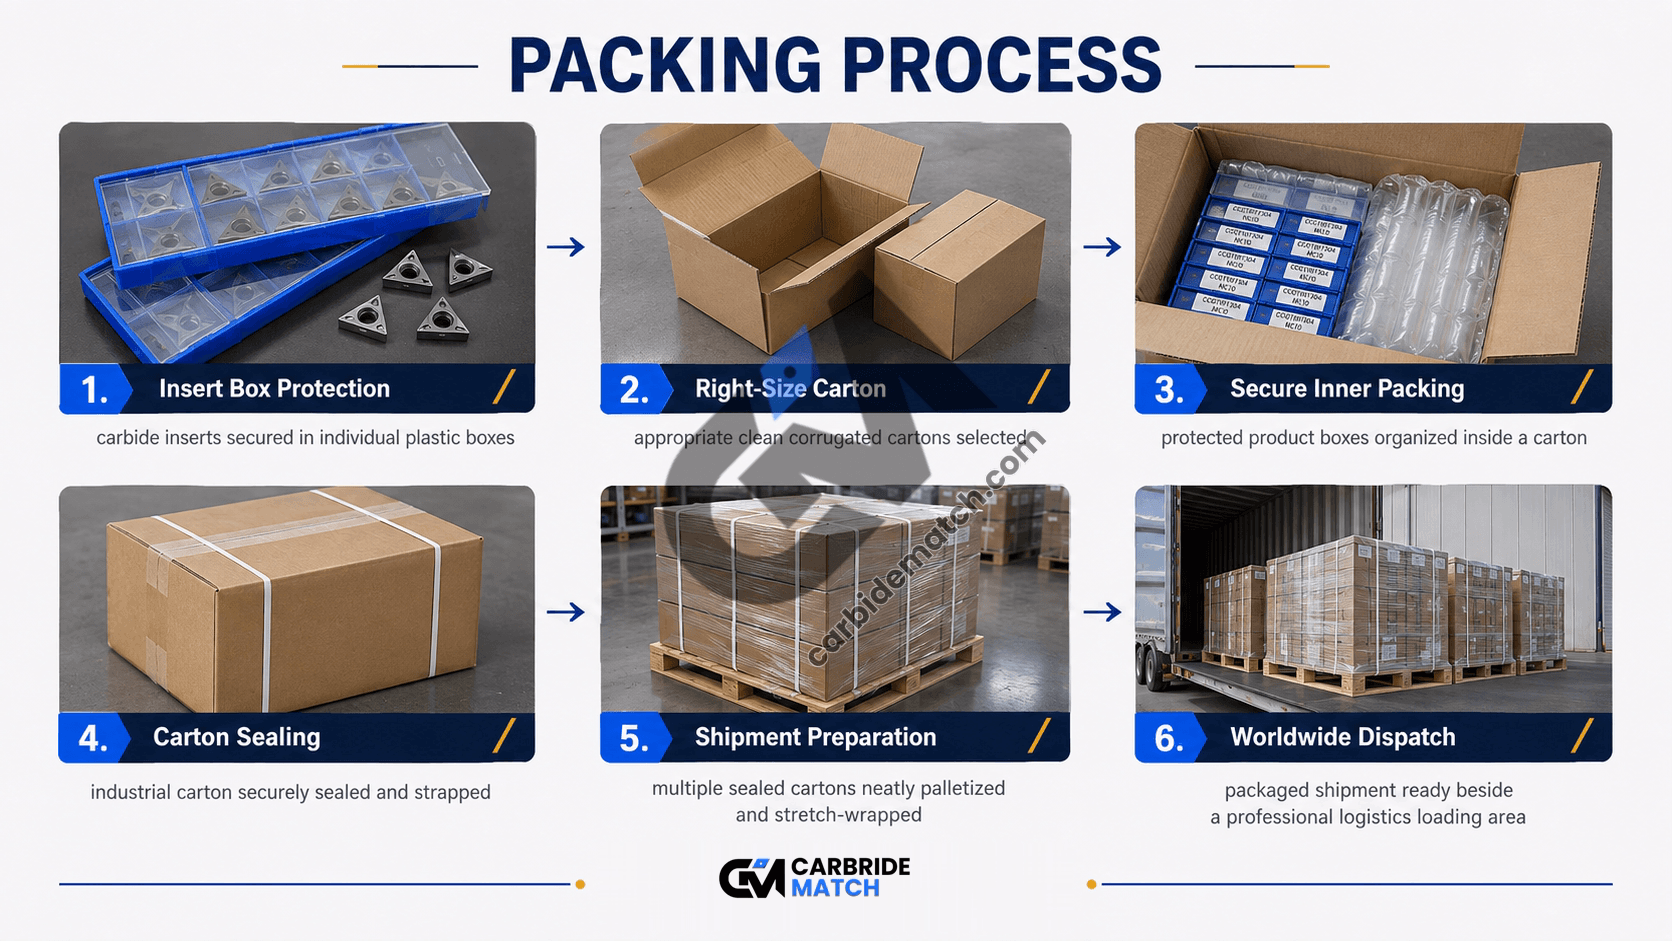
Customize insert markings and packaging to meet your order requirements.
Available WNMU Milling Insert Sizes
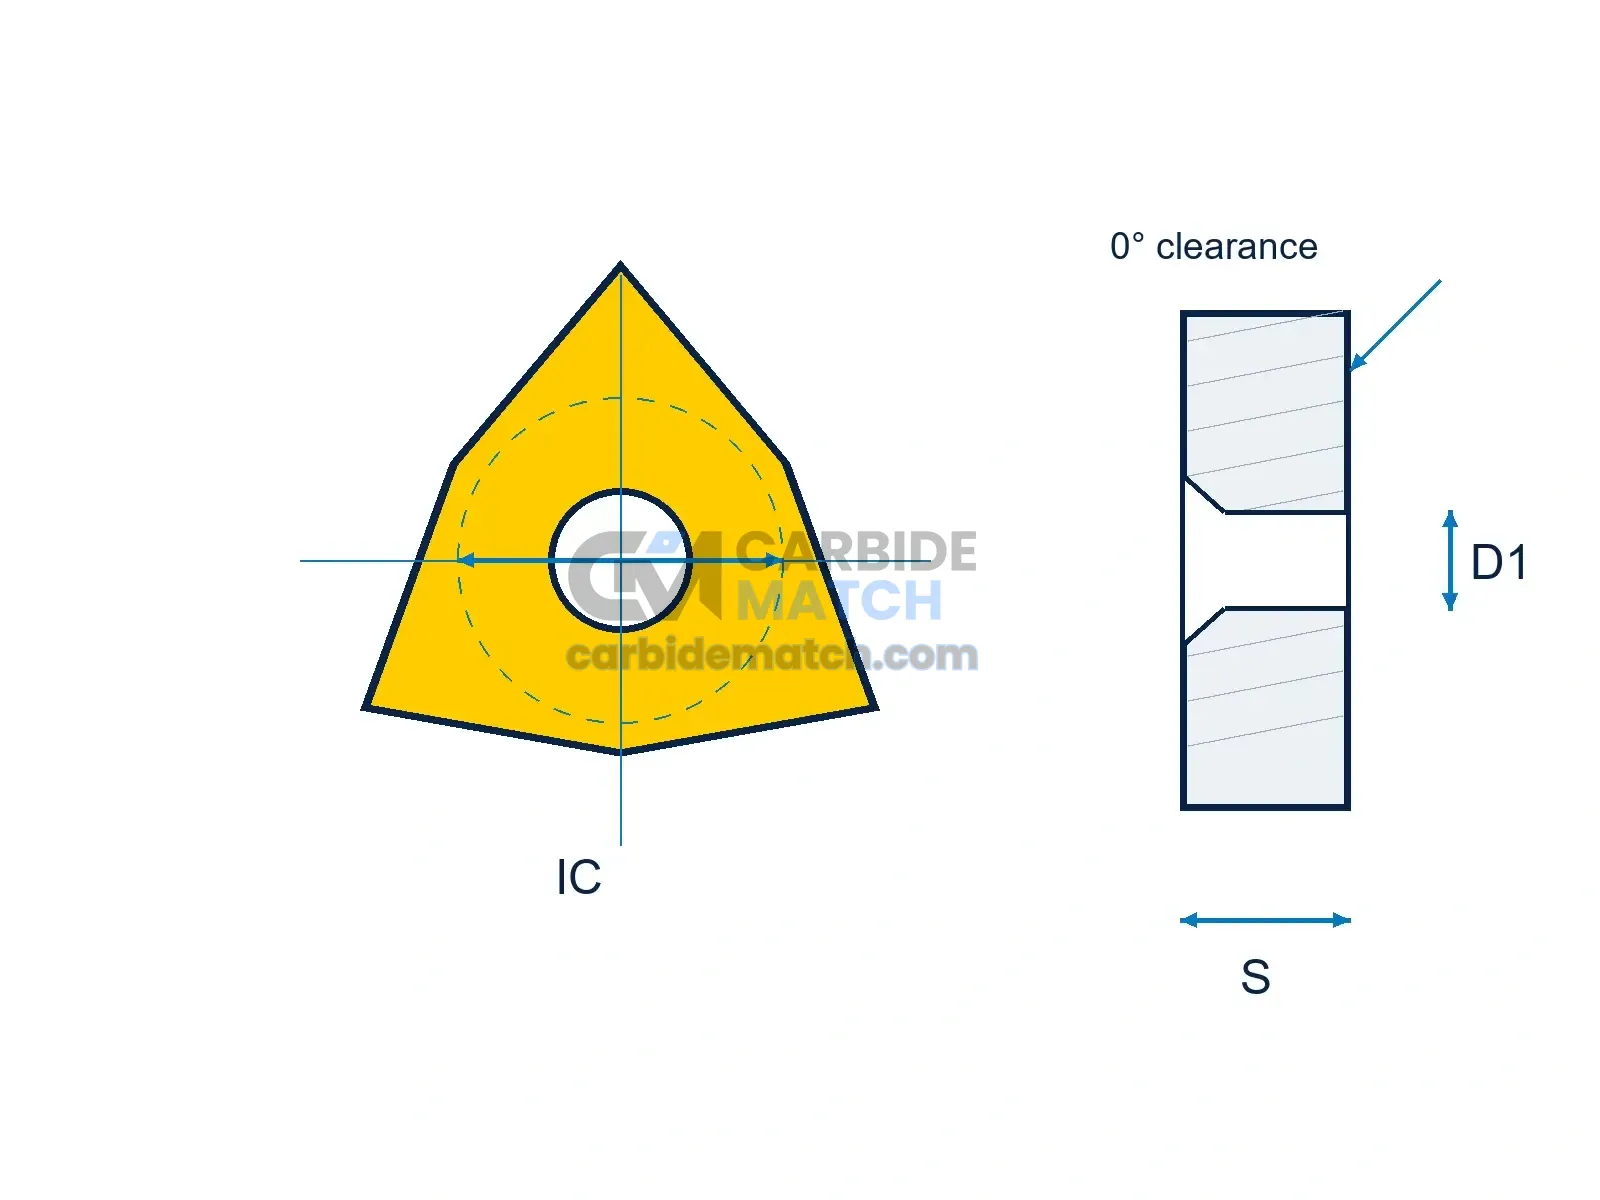
CarbideMatch manufactures WNMU inserts in the standard sizes listed below and can review custom dimensions and application-specific configurations. Send your required designation, cutter model, drawing, sample, work material or cutting conditions for technical review and a quotation.
ISO Designation
IC (mm)
S (mm)
D1 (mm)
RE (mm)
WNMU 040304EN
6.7
3.06
3.2
0.4
WNMU 050408-WL
8.8
4.2
Drawing required
0.8
WNMU 060408R
10.15
4.36
4.2
0.8
WNMU 080608-GL
12.48
6.45
4.7
0.8
WNMU 080608-GM
12.48
6.45
4.7
0.8
WNMU 080608-GH
12.48
6.45
4.7
0.8
WNMU 080608-WL
14.02
6.53
Drawing required
0.8
Don't See the Configuration You Need?
The configurations shown above represent commonly requested options and may not include everything we can supply. Contact us to check another specification or discuss your custom requirements.
Select the insert and cutter as a complete system. Review the operation, component geometry, machine rigidity and engagement before choosing the grade, coating and edge preparation.
Square-Shoulder Milling
Machines adjoining walls and floors using a cutter designed for the required shoulder accuracy.
Face Milling
Creates flat surfaces with suitable tooth pitch, cutter offset and edge engagement.
Slot Milling
Uses a compatible platform within its full-width cutting and chip-space limits.
Side Milling
Machines vertical surfaces with controlled overhang, runout and axial engagement.
WNMU Insert FAQ
Why is the WNMU080608 designation insufficient for replacement?
Different platforms use different IC, thickness, hole and underside contacts. Match the complete insert drawing and cutter model, including the suffix.
How should all six edges be tracked in production?
Use a consistent face-and-index sequence, log each used position, and inspect seating pads before rotating or flipping the insert.
What can cause a shoulder to taper despite correct programming?
Check cutter deflection, spindle runout, axial insert height, pocket damage, overhang and cutting-force variation along the wall.
How should screw torque be selected?
Use the torque for the exact cutter screw and lubrication condition; insert family, hole size and nominal insert size alone do not determine torque.
When does a finer tooth pitch reduce productivity?
It can restrict chip space or exceed power limits in deep slots, gummy materials or unstable engagement. Select pitch from the actual operation.
How can a replacement trial distinguish geometry from grade effects?
Hold geometry and edge preparation constant when comparing grades, then change one factor at a time while recording wear and component results.
About CarbideMatch
CarbideMatch is a cutting-tool manufacturer and multi-brand distributor with years of OEM manufacturing and industry experience. We currently focus on carbide and indexable inserts across a wide range of brands, grades and specifications.
Search by part number, ISO/ANSI code, grade or application to quickly identify suitable inserts and compatible alternatives